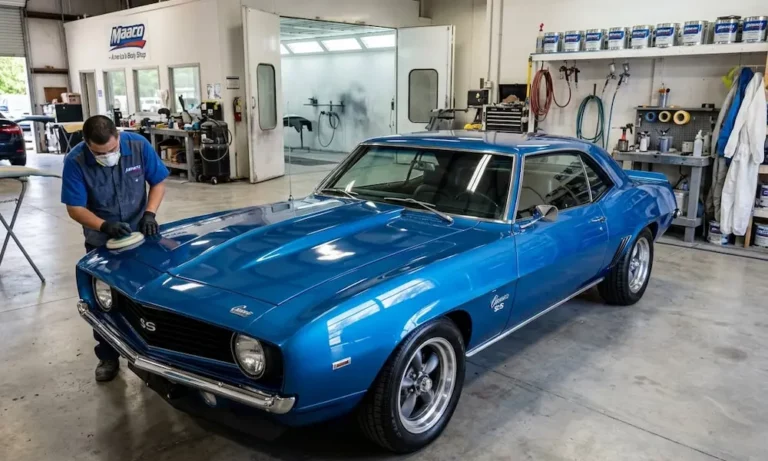
Got a door ding, a fresh respray, or a panel repair that needs to disappear? Learning how to blend in paint on a car is the difference between a repair that looks factory-fresh and one that screams “I’ve been in a crash.” This guide walks you through every step — from surface prep to clearcoat — so you can pull off a seamless finish. Stick around, because the details here really do matter.
What “Blending” Actually Means
Blending isn’t just spraying paint and hoping for the best. It’s a controlled optical fade — you’re tricking the eye into seeing one continuous, unbroken finish instead of a patched repair.
When done correctly, blending creates a gradual color transition that eliminates hard lines between new and old paint. The human eye can’t detect the shift because it happens over a wide gradient, not a sharp edge.
Here’s what you’re actually managing when you blend:
- Hue — the base color itself
- Value — how light or dark the paint appears
- Chroma — the intensity or saturation of the color
- Metallic orientation — the angle at which aluminum flakes reflect light
Miss any one of these, and the blend shows.
Know Your Paint System First
Before you touch a spray gun, you need to know what you’re working with. There are two main paint architectures, and they behave very differently.
Single-Stage Paint
Single-stage paint combines color pigments and protective gloss into one layer. It’s simpler to apply and great for classic car restorations and fleet vehicles. But it has a major flaw — you can’t sand or compound it without shearing off the tops of metallic flakes, which ruins the finish permanently. It’s also highly vulnerable to UV damage since there’s no protective clear layer on top.
Basecoat and Clearcoat (The Modern Standard)
This two-stage system separates color from protection. The basecoat handles the visuals. The clearcoat — loaded with UV absorbers and protective resins — handles durability and gloss. Because the metallic flakes sit safely under the clear, you can sand and polish the final surface without disturbing the color at all. This is the system you’ll use for virtually every modern vehicle repair.
Surface Prep: The Foundation of a Flawless Blend
Skipping prep is the fastest way to ruin a blend. Modern urethane coatings need a specific microscopic scratch profile to bond properly. Too coarse, and scratches telegraph through the finish. Too smooth, and the paint won’t stick.
The Abrasive Grit Progression
Work through this sequence methodically. Don’t skip grits.
| Abrasive Grit | What It Does | How to Apply |
|---|---|---|
| 80–180 | Strips old coatings, shapes body filler | Dry with dual-action orbital or rigid block |
| 220–320 | Featheredges paint perimeters, refines filler | Dry or semi-rigid block sanding |
| 400–600 | Preps for primer or solid color basecoats | Dry or wet mechanical sanding |
| 800–1000 | Final primer prep for metallic colors (prevents sand-scratch swelling) | Wet with soft interface pads |
| 1200–1500 | Scuffs surrounding clearcoat for adhesion | Wet or grey scuff pads |
| 2000–5000 | Removes post-paint defects, preps for polish | Damp machine sanding with foam interface |
Primer Selection
Body filler is porous and can’t be painted directly. You’ll need one of these primers to seal the repair:
- Epoxy primer — best adhesion for bare metal, excellent corrosion resistance
- Self-etching primer — bites into raw steel or aluminum for small spot repairs
- Sprayable polyester primer — fills wavy panels like liquid body filler
- Urethane primer surfacer — creates a workable, smooth layer for blocking flat
Always apply a guide coat — a thin mist of dark contrasting paint over lighter primer — before blocking. The dark coat stays in low spots and scratches, giving you a visual map of where you haven’t leveled yet.
Painting Plastic Bumpers
Plastic bumpers flex. Standard cured paint doesn’t. The result? Cracking.
You must add elastomeric flex additives — typically 10–20% by volume — to your primer, basecoat, and clearcoat when spraying flexible components. These plasticizers keep the cured film pliable enough to move with the bumper during impacts or temperature swings.
Also, raw plastic has low surface energy. It resists bonding. Apply a liquid adhesion promoter to the bare plastic before any primer. It acts as a chemical bridge between the plastic and the coating.
The static charge problem: Plastic holds intense static electricity. When metallic paint gets sprayed at a charged bumper, the static physically pulls the aluminum flakes into erratic orientations. On a grounded metal panel next to it, flakes lay flat. The bumper ends up looking darker or lighter — even with the same paint. Fix this with anti-static wipe-down fluids and an ionizing air gun immediately before spraying.
Color Matching: Don’t Skip the Verification Step
The factory paint code gives you a starting point, not a guaranteed match. UV exposure, environmental fallout, and plain aging shift the original color over time.
Using a Spectrophotometer
A multi-angle digital spectrophotometer reads the actual current state of the paint on the vehicle — not the theoretical factory formula. It measures hue, metallic flake concentration, pearl depth, and sun fade, then generates a custom micro-adjusted formula for your computerized mixing system.
Spray-Out Cards
Before spraying the car, mix the formula and apply it to a physical test panel called a spray-out card. Use the same gun, same air pressure, same number of coats you’ll use on the vehicle. Then hold the cured card against the car under daylight-simulation lamps.
The key check is the flop angle — how the paint looks from a sharp oblique angle versus straight on. A metallic color might match perfectly face-on but look completely different at a flop. If the flop doesn’t match, adjust your formula before touching the car.
Masking for a Seamless Edge
Good masking in blending isn’t just protection — it’s an active technique that controls how the paint transitions.
Eliminate the Hard Tape Line
Flat tape creates a raised edge. Multiple coats build up against it. When the tape comes off, you’re left with a cliff-like ridge that chips easily and needs aggressive wet sanding to remove.
Back masking (reverse taping): Apply tape from inside the panel gap outward with the adhesive facing up. Fold it back over itself. Paint hits the rounded fold and gently rolls under, creating a soft, tapered fade instead of a hard step.
Foam aperture tape: For gaps between panels, press a cylindrical foam rope into the gap. It expands to fill the void and creates the same rounded, soft edge.
Liquid masking: For honeycomb grilles, wheels, or complex trim that tape can’t wrap cleanly, spray-applied liquid masking polymer dries into a protective skin. Peel or wash it off after painting.
How to Blend in Paint on a Car: The Application Process
This is where the technique gets precise.
Staggering Your Basecoat Coats
Apply the first coat of color over the primer, extending just past the primer boundary. Each subsequent coat extends further outward — typically 4–6 inches for small repairs, 12–14 inches for large panels. This creates a descending gradient of film thickness.
As you spray toward the blend edge, arc the gun nozzle away from the panel while easing off the trigger. This deposits progressively less material at the outer edge. Never flick your wrist at the end of a pass — that causes uneven droplet distribution and visible paint lines.
Stopping the Halo Effect
The halo — a dark ring around the repair — is the most common failure when blending metallics. It happens because metallic flakes land on the dry, rough scuffed surface and stand on edge inside sanding scratches. Light gets trapped by the vertical flakes, making the perimeter look darker.
The fix is a wet bed technique. Before applying any color, spray a full coat of transparent, unpigmented basecoat resin (a blending solvent or basecoat blender) over the entire blend zone. This creates a fluid foundation. When metallic basecoat hits the wet bed, flakes sink in and lay flat — matching the orientation of the factory finish.
The Drop Coat
For the final basecoat pass, apply a drop coat: drop your air pressure by 5–10 PSI and double your distance from the panel. This delivers a fine, semi-dry mist that settles metallic flakes uniformly across the surface without disturbing the layers below. It kills tiger stripes and uneven banding in one controlled pass.
Tri-Coat Finishes: The Hardest Blend
Tri-coat pearl finishes have three layers: solid base, translucent pearl mid-coat, and clearcoat. Every extra mid-coat pass darkens the color permanently. You’re managing two separate, overlapping blend fields.
Industry standard: minimum 24-inch blend allowance for tri-coats versus 12 inches for standard two-stage colors. Trying to compress a tri-coat blend into a small corner will always result in visible banding.
Clearcoat: The Rule Everyone Gets Wrong
Here’s the big one: you cannot blend clearcoat in the middle of a panel. Full stop.
Attempting to melt clearcoat into the old paint with a fade-out solvent creates a tapered edge where film thickness drops toward zero. At that point, there’s no UV protection in the resin. Within months, the edge will oxidize, turn white, and peel. All major paint manufacturers void the warranty on clearcoat blends on exterior panels.
The only correct method: apply clearcoat from one panel edge to the opposite edge, encapsulating the entire substrate in a full-thickness, uniform protective layer.
Clearcoat blending solvents are only acceptable for interior door jambs, hidden pillars, or roof rails with minimal sun exposure.
Choosing the Right Clearcoat Solids Level
| Clearcoat Type | Solids Content | Best For |
|---|---|---|
| Low Solids (LS) | 30–40% | Budget work; rarely used in collision repair |
| Medium Solids (MS) | 40–50% | High-volume shops; forgiving to apply |
| High Solids (HS) | 50–65% | Premium repairs; better gloss and UV resistance |
| Ultra-High Solids (UHS) | 65%+ | Show cars; maximum durability and chemical resistance |
High solids clearcoats shrink less during curing, producing a deeper, more mirror-like finish. But their thick viscosity demands precise technique and temperature control to avoid orange peel.
Environmental Controls: Paint Booths and Defects
The optimal spray environment is 68–77°F with humidity below 60%. Outside these parameters, defects are almost guaranteed.
| Defect | Cause | Fix |
|---|---|---|
| Blushing (milky haze) | High humidity; moisture condenses in wet clearcoat | Slow reducers; dehumidified, climate-controlled booth |
| Dry spray / orange peel | High heat; solvents flash before paint levels | Drop air pressure; slow-grade reducers; reduce gun distance |
| Solvent pop (pinholes) | Excessive film build; clearcoat skins over trapping solvents | Proper flash times between coats; regulate booth temp |
| Edge mapping / ringing | Hot solvents bite into uncured primer or filler | Fully cure and outgas substrate layers before topcoating |
Post-Paint Care and Curing
A heated booth makes the exterior shell dust-free in hours, but internal chemical cross-linking continues for weeks. During this outgassing phase:
- No high-pressure automatic car washes
- No stiff brushes or harsh alkaline detergents
- No carnauba wax, polymer sealants, or ceramic coatings
If you apply a ceramic coating over paint that’s still outgassing, the impenetrable ceramic layer traps solvents beneath the surface — causing solvent pop, bubbling, and complete adhesion failure of both the clear and the ceramic.
Wait 30–60 days after painting before applying any ceramic coating. Once applied, keep the vehicle dry for 24–48 hours. The ceramic reaches full hardness in 7–14 days.
FAQs About How to Blend in Paint on a Car
How do you fix dust nibs in clearcoat without repainting?
Once the clearcoat cures, use 2000–3000 grit wet sandpaper to level the nib flat. Then polish the matte spot with a cutting compound on a dual-action polisher. The gloss comes back completely and no repainting is needed.
What’s the purpose of a guide coat during primer sanding?
A guide coat is a thin layer of contrasting dark powder or spray applied over the primer. As you block sand, the abrasive removes it from high, flat areas first. It stays in low spots, pinholes, and deep scratches — giving you a precise visual map of where the surface isn’t level yet.
Can you mix waterborne and solvent-borne paint systems on the same repair?
Yes, but only in sequence — never in the same gun. Apply waterborne basecoat first, then dry it with high-velocity air movers (water needs airflow to evaporate, not just heat). Once the basecoat is fully matte and dehydrated, seal it with a solvent-borne two-component clearcoat. Mixing the liquid paints themselves will instantly destroy both products and your equipment.